A buyer's guide to specifying leather loafers for OEM and private-label production: how last shape, lining, sole construction, and hide selection decide what your order actually delivers, plus a five-point bulk QC checklist and the reference pack to send a factory before sampling.
OEM / ODM Sourcing Guide
Three decisions decide what a leather loafer becomes before a single pair is cut: the last it is built on, how the upper is lined, and how the sole is attached. Cost discussions usually come later, but changing any one of these three after the last is approved means new patterns, new samples, and a restart. Buyers who fix them in writing at the start — references, size grid, branding — get fewer surprises at bulk.
- The last defines both fit and silhouette; almond and apron toes are different lasts, not a decorative option.
- Full leather lining is the premium, breathable default; partially lined builds are a cost and weight tier.
- Cemented and stitched soles differ in flexibility, resoling and how the shoe reads on shelf.
- Matched-hide cutting is the only reliable way to keep left/right grain and shade consistent.
- Send a reference loafer, your size grid and branding files before sampling — not after.
Why the last is the first thing to sign off
A loafer has no lacing to absorb error. On an oxford or derby you can tighten, loosen, or adjust the tongue; on a loafer the upper either grips the foot or it does not. That makes the last the highest-risk item in the whole order, and it also sets the look: toe shape, heel profile, and how full the shoe reads across the instep all come from the last, before any leather is chosen.
Almond versus apron or round toe
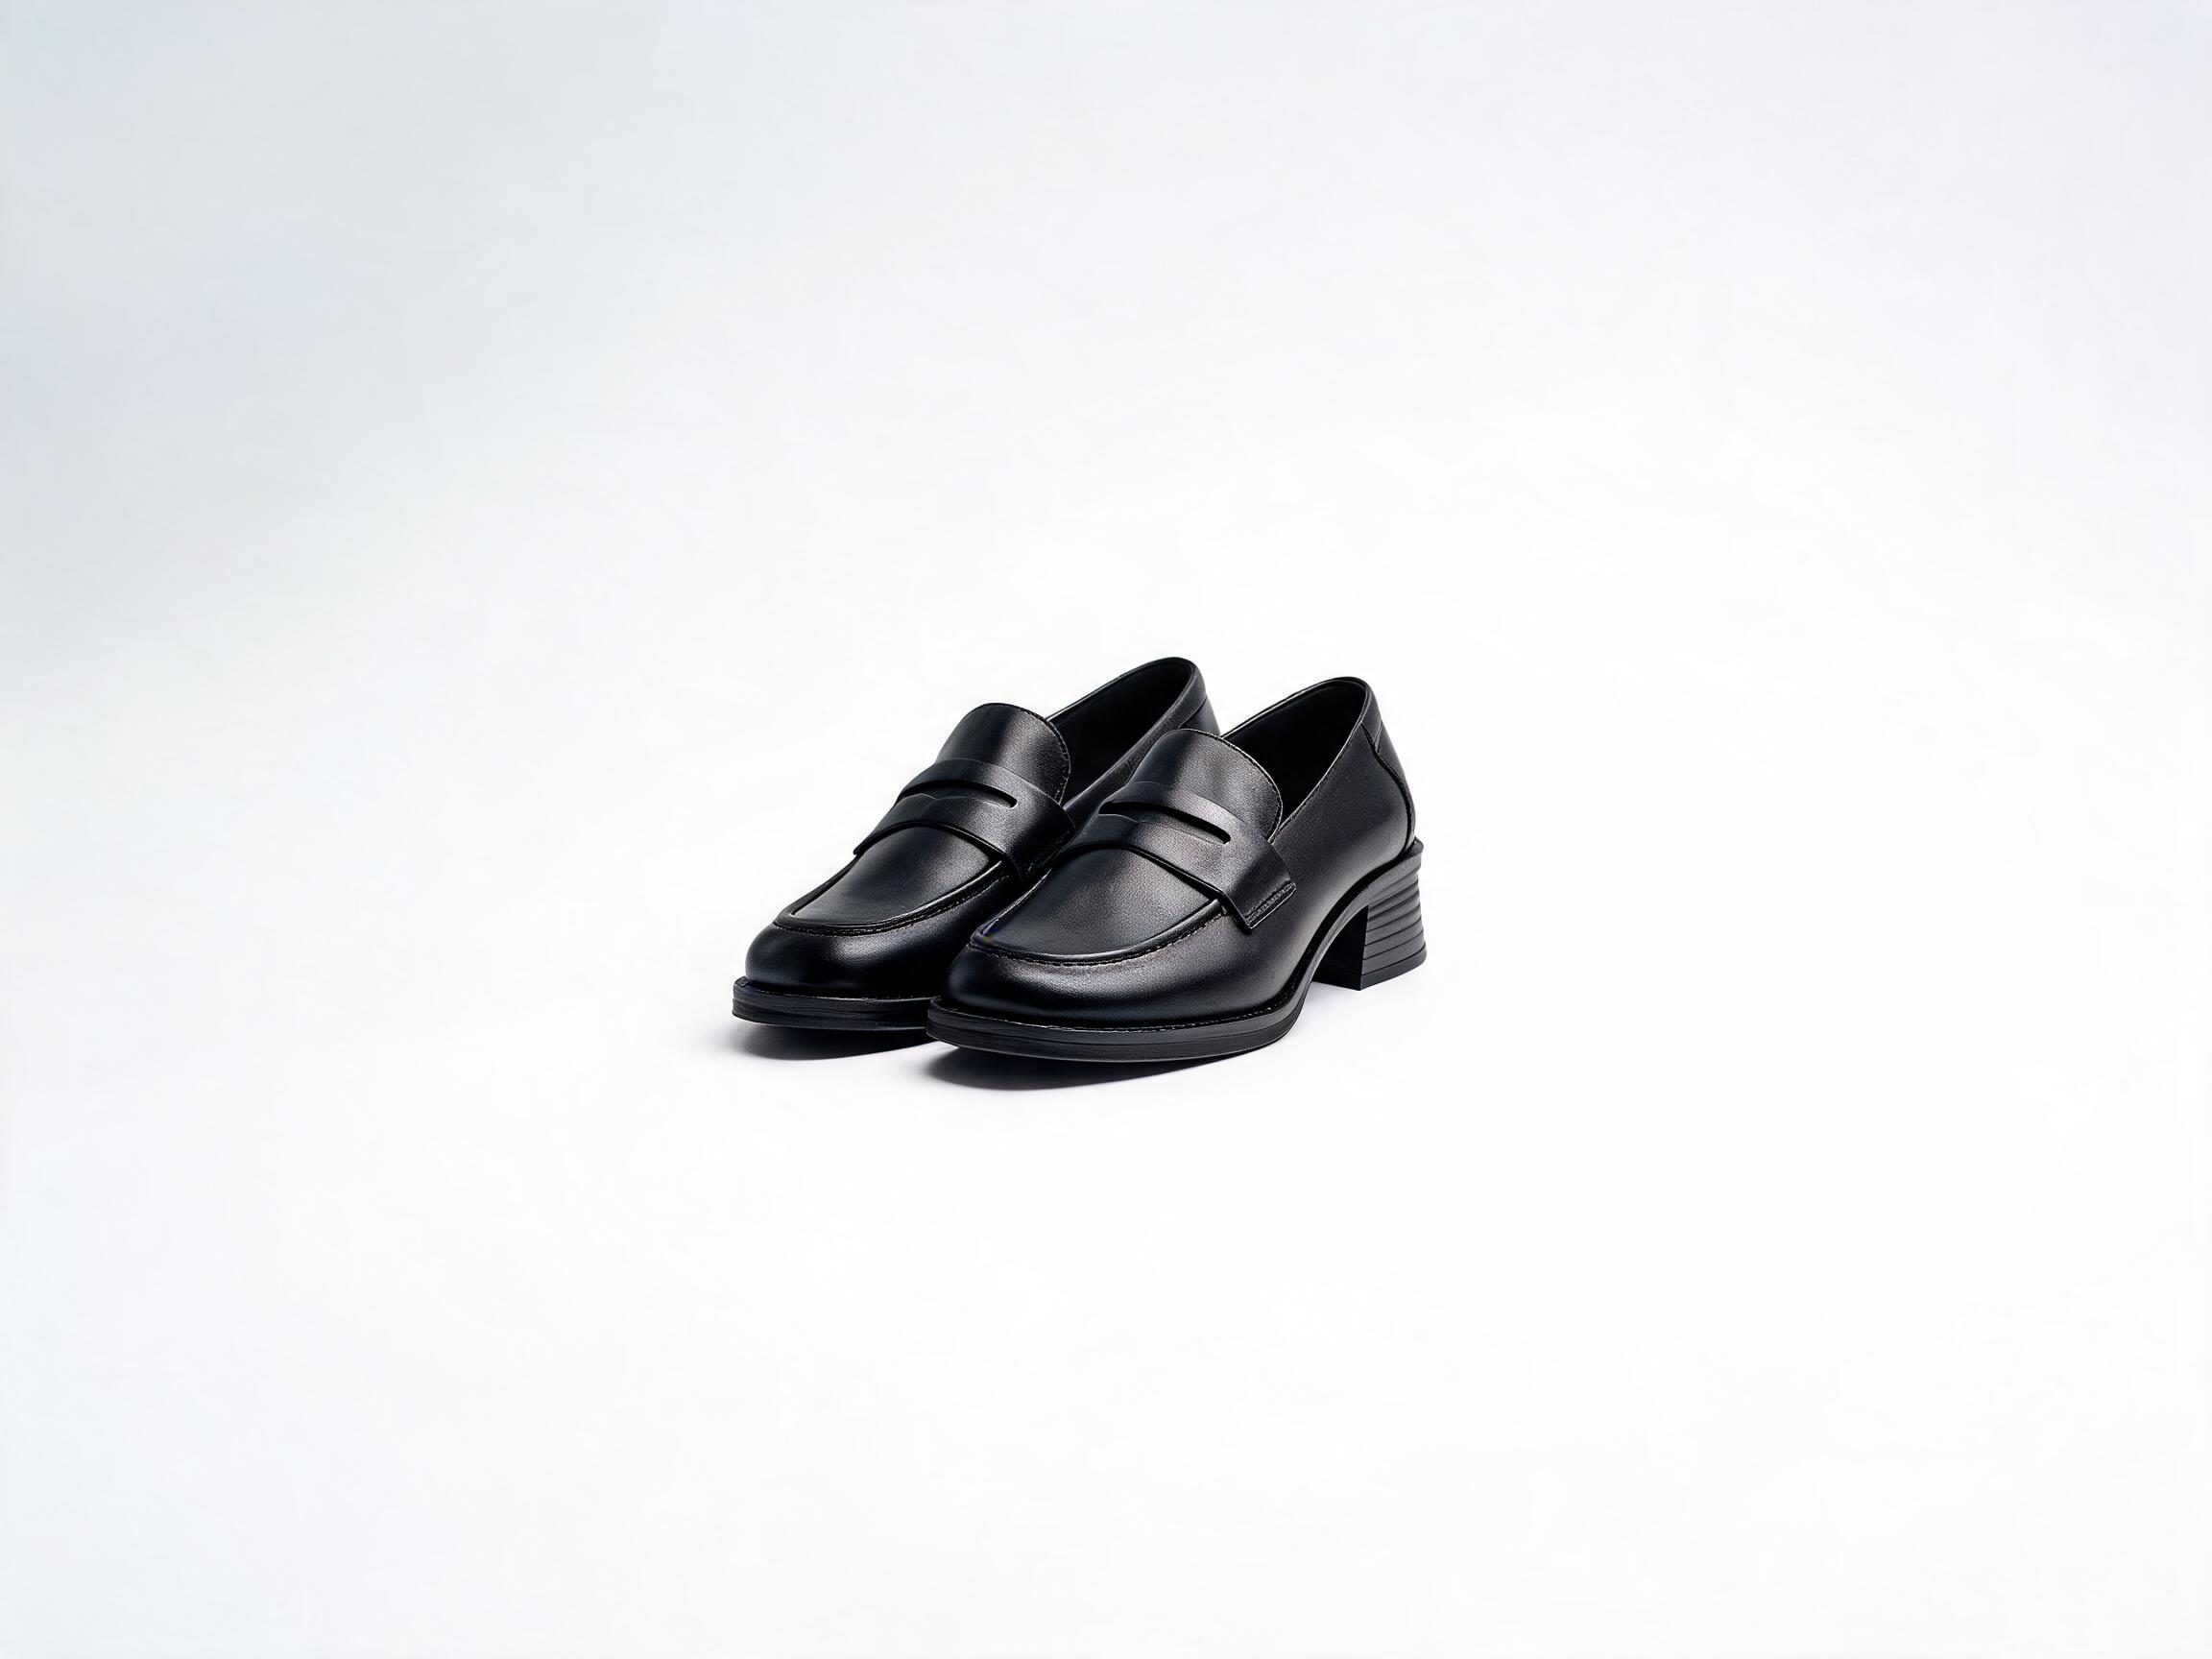
An almond toe is a tapered, slightly pointed last. It reads dressier and works well for women's labelled programmes where the silhouette needs to stay slim through the forefoot. The Black Leather Loafers are built on an almond last with a low block heel and a rubber outsole in cemented construction — a shape that suits uniform, retail and premium casual ranges where the toe should not look bulky.
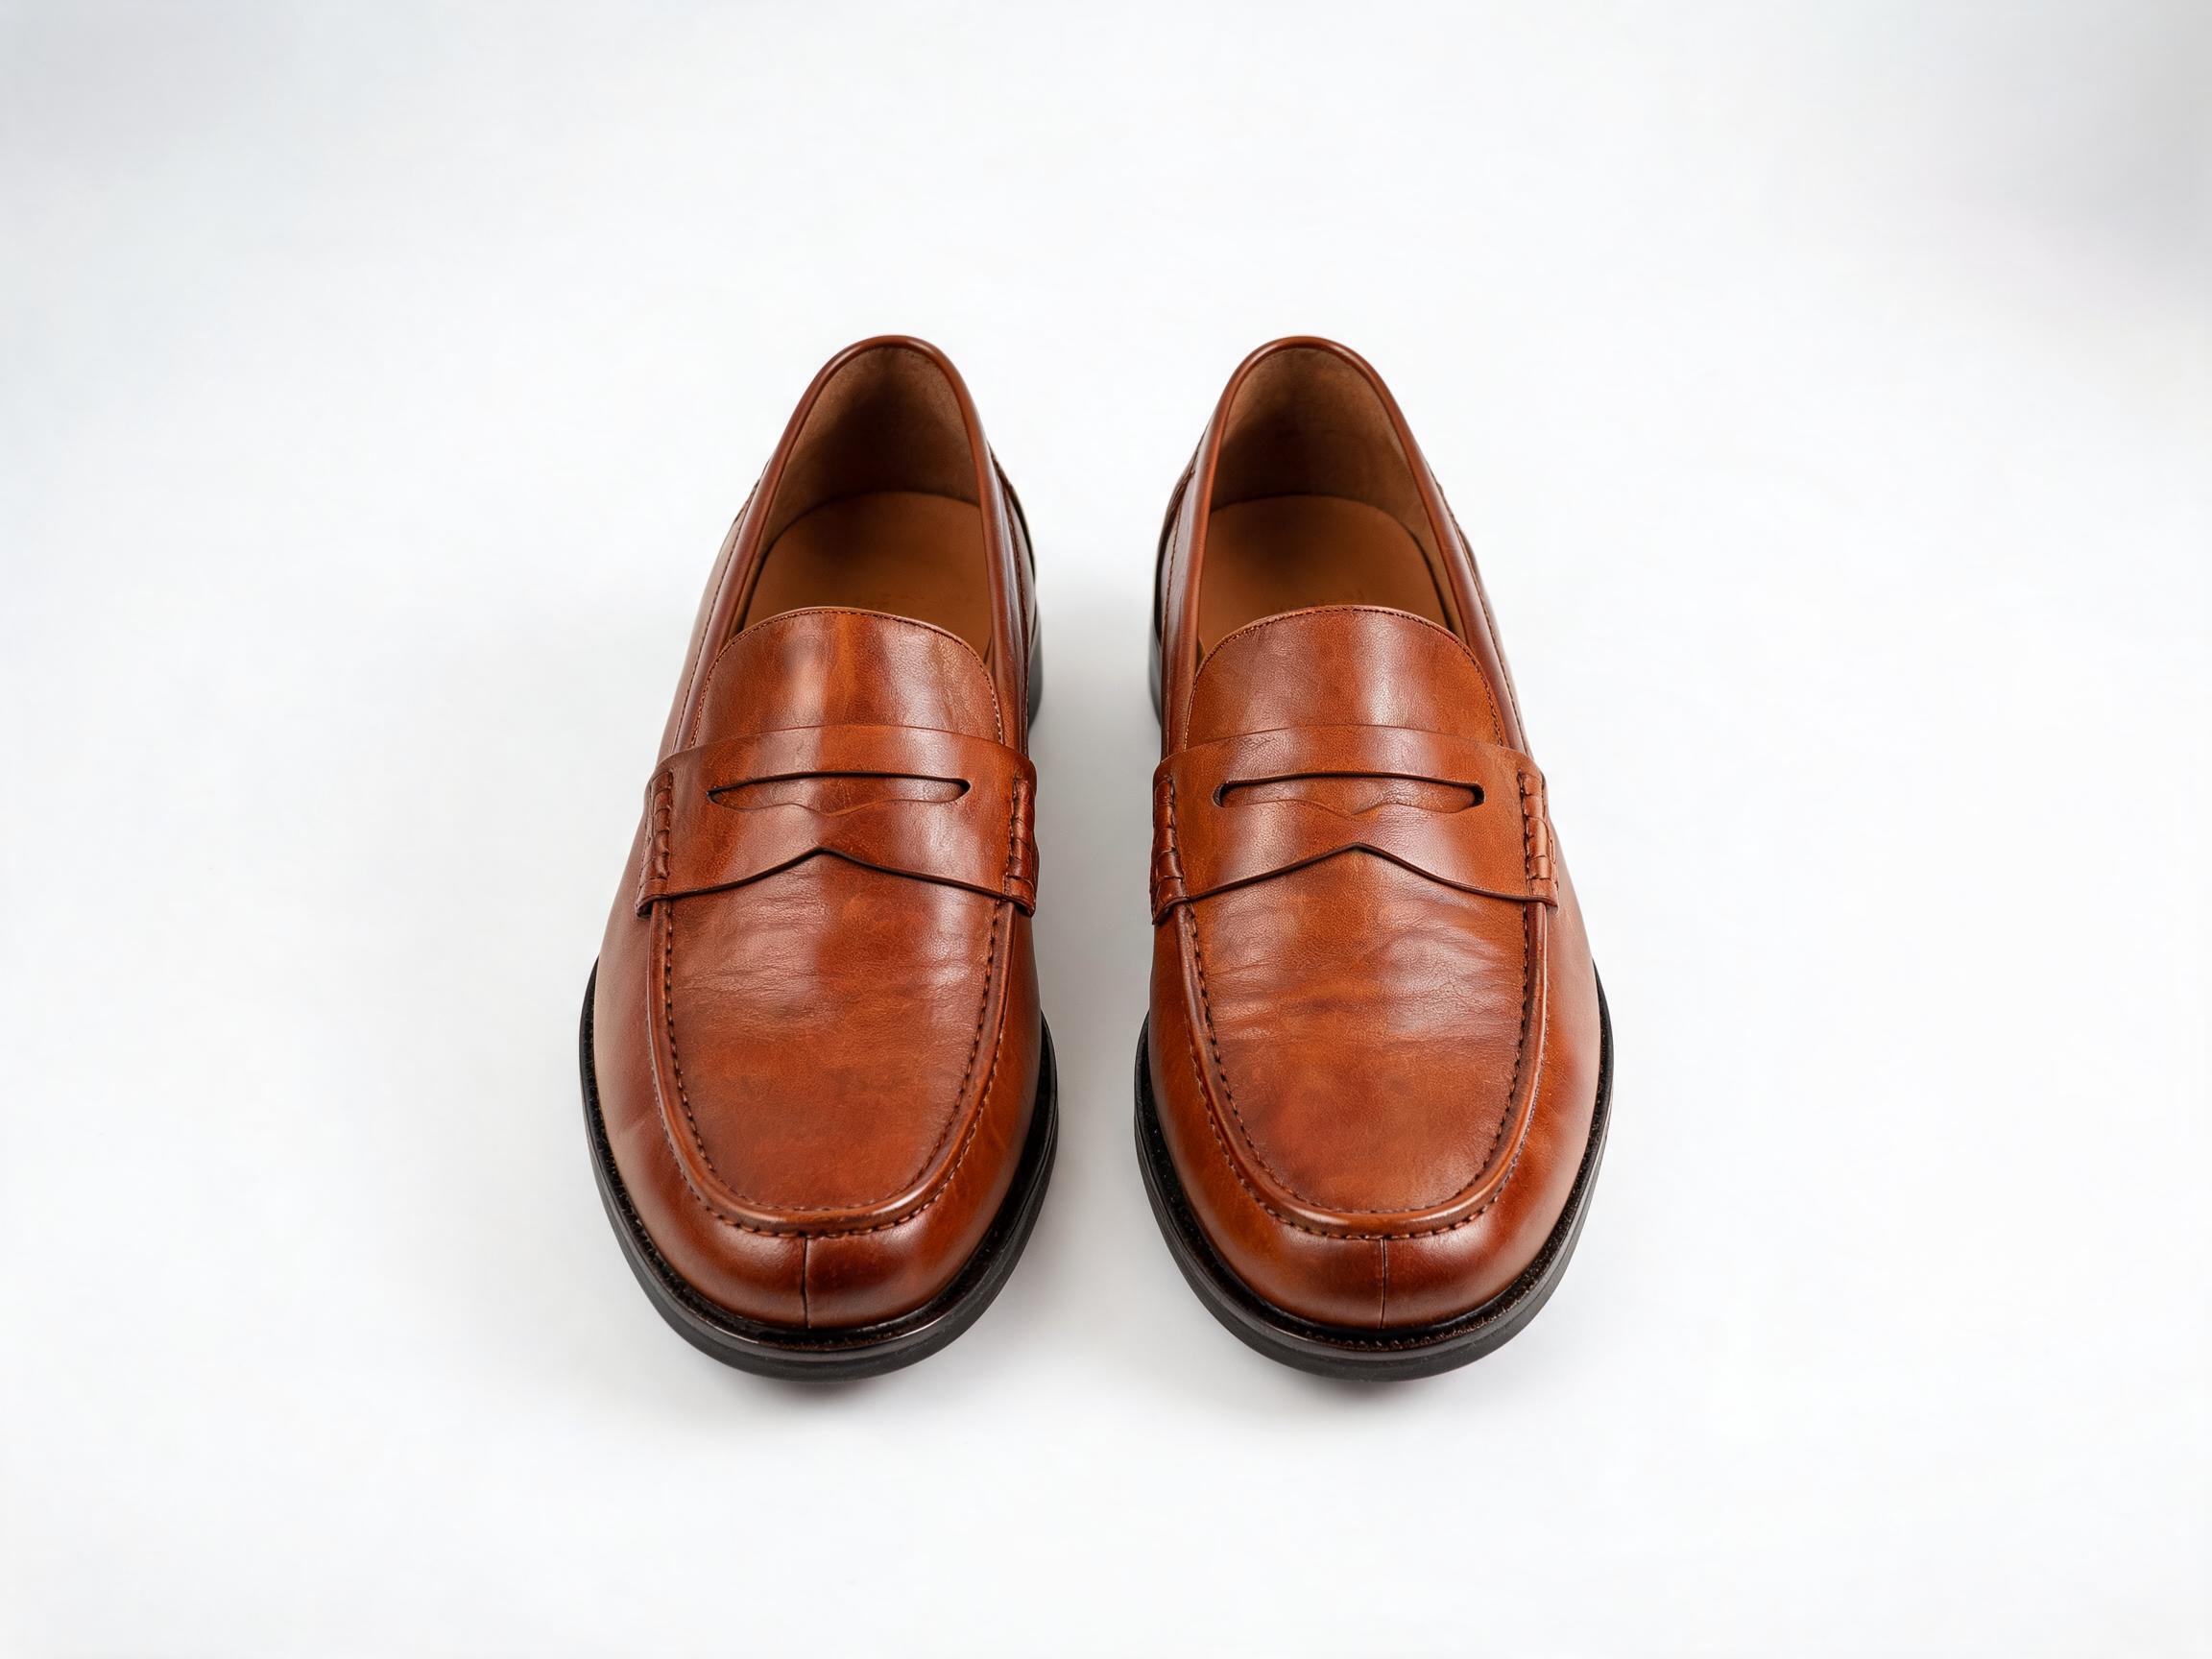
An apron toe last is fuller and more rounded, with the apron seam running across the front. It is the classic men's slipper shape and it photographs heavier, which is often what buyers want in a heritage or smart-casual line. The Cognac Penny Loafer Shoes use an apron toe on polished full-grain leather, with the penny strap and a hand-stitched detail giving the upper its character.
Slimmer or fuller girth
Girth is the measurement buyers forget to specify. Two loafer lasts can share the same length and be very different across the ball of the foot and the instep. A slimmer girth flatters on shelf but can run tight after a long day; a fuller girth fits a wider market but can look shapeless if the toe is rounded too far. When briefing a factory, give the target market and, where you have it, your historic size curve, then ask two questions rather than one:
- What girth does the proposed last give at the ball and instep, and how does that compare with the last I am currently selling?
- If we need to widen or narrow, does that mean a new last, a new pattern, or both?
Which of these applies to your programme is a question to confirm with the supplier against your reference shoe, not something to assume from a photo.
Lining: where the season and the price tier are set
Lining is the second lever, and it is the one that most changes how a loafer feels after an hour of wear. It also changes the cost of the upper, the weight of the shoe, and how the shoe handles a hot or cold selling season.
| Lining approach | Typical effect on wear | Where it fits |
|---|---|---|
| Full leather lining (forepart, heel and tongue area) | Breathable, holds shape well, premium hand-feel when the foot goes in | Upper-tier retail, year-round ranges, buyers who lead on leather content |
| Partially lined (forepart or heel only) | Lighter upper, more flexibility in the vamp, cooler in warm-season lines | Cost-engineered programmes, lightweight or summer capsules |
Both of the products here use soft leather lining, which is the natural choice when leather is the selling point. If you are building a warm-weather range, a partially lined build can be the right call — but confirm with the factory how the lining decision interacts with the last and the sole before you price the order, because an unlined vamp often needs a different pattern allowance.
Insole and footbed specification sits alongside lining. A cushioned insole with a leather footbed, as used on the Cognac Penny Loafer Shoes, gives a firmer, more traditional feel; a cushioned insole on the women's loafer gives more immediate softness underfoot. Neither is better in the abstract — the question is which one matches the retail price point and the customer's expectation.
Sole construction: cemented versus stitched
These two methods are the main choice for leather loafers, and they change flexibility, resoling and the formal register of the shoe.
| Consideration | Cemented construction | Stitched construction |
|---|---|---|
| Flexibility out of the box | Softer and quicker to break in | Stiffer initially; softens with wear |
| Resoling | Sole is bonded to the upper; resoling depends on the cobbler and the bond | Typically more straightforward for a repair specialist |
| Formality and visual weight | Lighter, cleaner edge; reads modern or casual | Visible stitching; reads more traditional and heavier |
| Example in range | Black Leather Loafers (cemented, rubber outsole) | Cognac Penny Loafer Shoes (stitched rubber sole) |
Note what the two products also show: sole material and sole attachment are separate choices. Both feature rubber outsoles, but one is cemented and one is stitched. Decide attachment first, then the outsole material and tread, then the heel. If you are unsure which attachment suits a specific retail price and use case, ask the factory to sample both on the same last so the comparison is fair.
Leather selection and matched-hide cutting
Once the last and the sole are fixed, the leather is what the customer actually sees. Three things matter most for a bulk order:
- Hide selection. Full-grain leather keeps the natural surface and shows grain; corrected or polished finishes give a more uniform face. The Cognac Penny Loafer Shoes use polished full-grain leather, and the Black Leather Loafers use polished calf leather — both are chosen for a clean, consistent face across a run, which is usually what retail buyers want when colour and grain must match on shelf.
- Matched-hide cutting. The left and right shoe of a pair should be cut from leather of compatible grain and shade. Ask the factory to confirm that left and right upper components are cut from adjacent or matched areas of the same hide, or from hides selected together. This is the single most effective control against a pair that looks mismatched in daylight.
- Finish and shade control across sizes. A colour that matches in the sample can drift between cutting batches, and small sizes and large sizes consume leather differently. Ask how shade is controlled between the first and last size in your grid, and how the final colour is approved — against a physical standard, not a screen.
Bulk QC checklist for leather loafers
Most inspection points for loafers are visual, but they need a fixed order so a five-minute check per pair stays consistent across a full run. Work through the pair as a unit, then check the pair against its neighbours in the carton.
- Grain and shade matching. Compare the left and right shoe in daylight. Check the pair against the approved standard and against the carton next to it, not only against the pair itself.
- Stitching. Look along the apron, the penny strap and the top line for skipped, uneven or wavy stitches and for thread-end trimming.
- Lasting wrinkles. Check the vamp and the sides where the upper meets the sole. Light, even creasing is normal in a leather upper; sharp diagonal wrinkles near the toe or the heel seat usually mean the upper was pulled unevenly.
- Sole bonding and edges. On cemented builds, look for a clean, even edge with no gaps or glue lines. On stitched builds, check that the stitching is consistent around the sole and does not cut into the upper.
- Forefoot flex points. Flex each shoe by hand along the natural ball line. The upper and the sole should move together without a hard break or a crack at the toe cap.
Where a defect depends on the pair the buyer will actually receive — colour approval, girth feel, finish gloss — the sample and the bulk run should be compared by the same method. If your quality team works to a written specification, share it with the factory before production, not at final inspection.
What to send the factory before sampling
The fastest way to avoid a re-sample is to send a complete reference pack with your first enquiry. For loafer programmes, that pack usually includes:
- A reference shoe or a clear technical drawing. A physical reference is best because the factory can measure girth, heel height and toe shape directly rather than inferring from a photo. If you can only send images, include side, top, sole and heel views.
- Your size grid. Specify the market (EU, UK, US) and the size range you sell. Both products here sit in defined ranges — EU 35–41 for the women's loafer and EU 39–45 for the men's penny loafer — and your grid tells the factory how to grade the pattern for your market.
- Branding requirements. Logo placement, embossing, label type, packaging and any private-label marks. Confirm which of these the factory can execute and where the cost sits — in the upper, the insole or the box.
- Target market and price tier. This lets the factory recommend lining and sole options that actually fit the retail position, instead of offering the premium build by default.
- Your quality expectations in writing. Colour matching standard, acceptable stitching tolerances, sole bonding criteria — anything you will reject at bulk should be listed before sampling.
Working with a loafer manufacturer on OEM and private-label terms
Aurevia Footwear Co., Ltd. is a B2B footwear manufacturer and exporter founded in 2011 and based in Quanzhou, China, with a 260-person team, in-house design and pattern teams, and OEM/ODM and private-label support. Inspection runs in multiple stages — incoming material, in-line, and finished shoe — with inspection reports shared on request, and third-party inspection is welcome. The company exports to Europe, North America and the Middle East.
For loafer programmes, the practical next step is to send your reference shoe, size grid and branding requirements, then ask the factory two questions before sampling: which last best matches your reference, and which lining and sole build fits your target retail price. Both answers should come back with a sample you can flex, measure and approve against your own standard.